Every lens that breaks or fails a quality check costs the lab more than the price of the material. The job must go through production again. This takes up more machine time, adds work for staff, and may require faster, more expensive shipping. If the defect is only found after the order has left the lab, it can also cause a customer complaint, an unplanned remake, and a longer wait for the patient.
Some lens breakage is a normal part of optical manufacturing and cannot be removed completely. However, consistently high defect or remake rates usually point to a problem somewhere in the production process. In my experience, the challenge is often not knowing that breakage is happening, but identifying exactly where and why it is happening. Common causes include incorrect machine settings, poor handling, unsuitable materials, missed maintenance, and gaps in the production data.
To reduce lens defects and breakage, labs need consistent processes and reliable production data. That means recording where failures occur, understanding what caused them, and using that information to stop the same issue from recurring. Here are the main areas to focus on.
Start by Defining What Counts as a Defect
Before a lab can reduce defects, it must first record them in a clear and consistent way. If one employee records a scratched lens as “operator damage” and another records the same issue as a “surface defect,” the lab’s reports will not show an accurate pattern. The same problem happens when categories are too general. Labels such as “breakage” or “failed quality control” confirm that something went wrong, but they do not explain what caused it or where it happened.
For the data to be useful, labs need a standard set of defect, breakage and remake reason codes across for every stage of production. Staff should use the same code when recording the same type of problem, regardless of their role, shift, or department. These codes may include:
- Incorrect lens or material selection
- Prescription or calculation errors
- Blocking failures
- Generator or polishing damage
- Coating defects
- Scratches and handling damage
- Chipping during edging
- Axis, size, or shape errors
- Mounting damage
- Equipment-related breakage
- Incorrect measurements
- Failed final inspection
- Customer-requested changes
- Supplier or material defects
The categories should be specific enough to support useful analysis without making the recording process unnecessarily complicated.
It is also important to distinguish between internal defects, customer changes, prescription changes, and warranty remakes. If every repeated job is placed in the same category, the lab may appear to have a production problem when the cause sits elsewhere.
Establish an Accurate Baseline
Once everyone is using the same defect categories, the lab can measure its current performance more accurately. To calculate a basic defect or breakage rate, divide the number of lenses recorded with the relevant defect or breakage by the total number of lenses produced during the same period. For example, if 50 lenses are recorded as defective or broken out of 5,000 produced, the defect rate is 1%.
This overall percentage gives the lab a useful starting point, but it does not explain where problems are happening or what is causing them. To find areas for improvement, the results need to be examined in more detail. Depending on the data available, labs can break the results down by:
- Production stage
- Lens material
- Lens design
- Coating or treatment
- Machine
- Production line
- Shift
- Operator or team
- Supplier
- Customer
- Prescription range
- Lab location
Looking at the data in smaller groups can uncover problems that the overall rate does not show. A lab might have an acceptable total breakage rate while still experiencing repeated failures with one machine, production process, lens material, or shift.
Use the same reporting period and calculation method each time you measure performance. Avoid changing them after improvement work begins, as this makes it harder to compare results and determine whether defect and breakage rates have actually improved.
Track Every Lens Through Production
A lab cannot investigate a defect properly if it does not know what happened to the lens before the problem was found.
A traceable production record can help show how a job moved through the lab, including:
- When it entered each production stage
- Which equipment or production processes were involved
- Which settings or programs were used
- Which employees handled or inspected it
- What materials and batches were involved
- Whether the job was held, rerouted, or reprocessed
- Where and when the defect was identified
- What corrective action followed
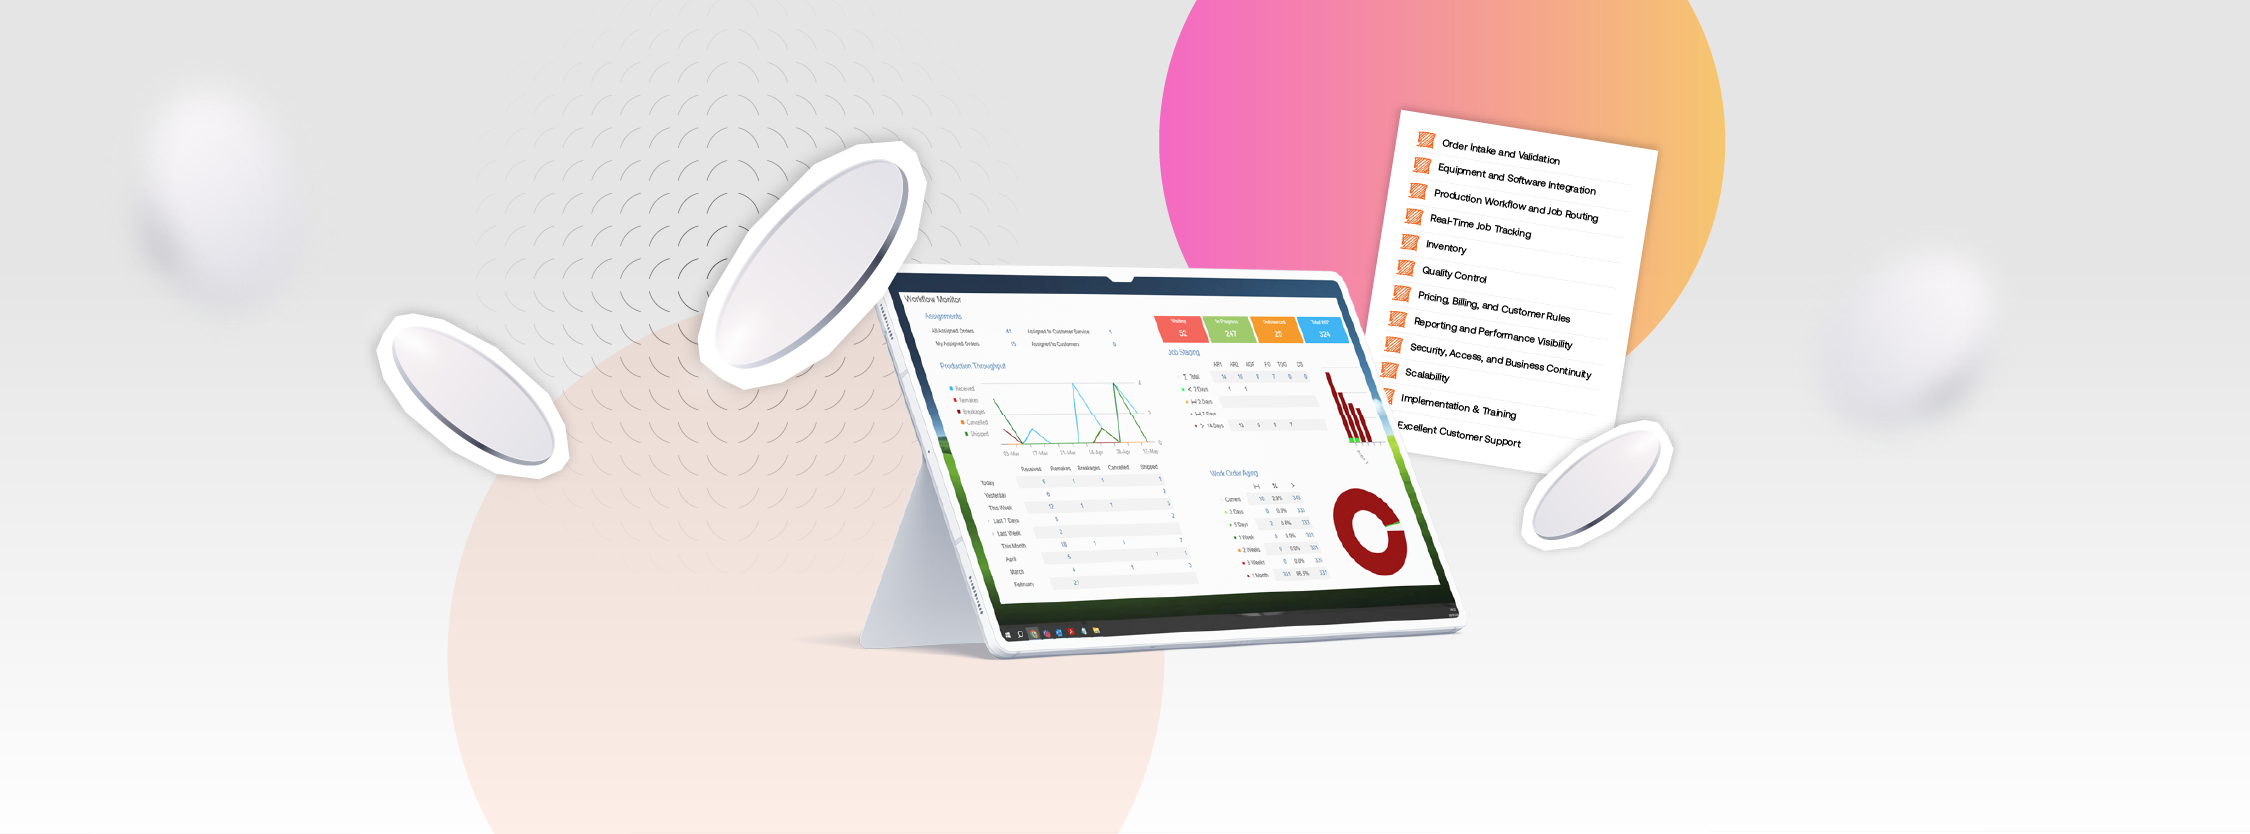
Barcode or tray tracking can make this information easier to capture without adding substantial manual work. The right LMS can also provide real-time lab tracking and reporting, helping managers identify repeated failures and production delays more quickly.
Tracking each lens throughout production makes it easier to tell the difference between a one-time accident and a recurring process problem. For example, if several chipped lenses passed through the same edger, the equipment or its settings become an obvious area to investigate. If scratches repeatedly appear at the same point in the workflow, the handling or production process at that stage may require attention.
When production and quality information can be viewed as part of the same workflow, managers have a clearer picture of where problems are occurring and where corrective action may be needed.
Find the Stage Where the Defect Began
A defect may be found at one stage of production even though it was caused much earlier. For example, a lens that fails its final inspection could have been damaged during blocking, polishing, coating, mounting, or transportation between departments. If the lab records every rejected job as a final-inspection problem, the reports will point to the wrong part of the production process.
Whenever a defect is found, record where it was discovered, but also look back through the production process to identify where the problem most likely began.
To make this possible, add clear inspection points throughout production. Do not wait until the final quality check to examine the lens. Inspect it after any stage where mistakes, damage, or changes in quality are likely to occur.
Finding defects earlier prevents the lab from spending more time, labour, and materials on a lens that cannot be completed successfully. It also makes it easier to trace the problem back to its true source and take the right corrective action.
Strengthen Incoming Material Checks
Some defects begin before the materials even reach the production floor.
Lens blanks, consumables, frames, and other supplies may arrive damaged, labelled incorrectly, or outside the required specifications. If staff do not find these problems when the delivery arrives, the materials can enter production and cause failures that appear to be the lab’s fault.
For this reason, incoming materials should be checked according to the level of risk they present. Expensive products, unfamiliar materials, and supplies connected to earlier quality problems may need a more detailed inspection. Lower-risk items can go through a simpler check, provided the lab continues to monitor their quality over time.
The receiving process should confirm:
- Product and material type
- Quantity
- Labelling and identification
- Batch or lot information
- Visible damage
- Storage requirements
- Relevant dimensions or specifications
- Supplier documentation where required
Supplier-related defects should be recorded by product and batch. This gives the purchasing team evidence when discussing recurring problems and helps the lab decide whether specific materials need additional inspection.
Connecting quality records with lens and material inventory controls can also help the lab trace affected batches, monitor stock movement, and prevent unsuitable materials from being used in additional jobs.
Review Storage and Material Handling
Correct storage and handling can help the lab prevent damage before production starts. Lens blanks and coatings materials can be affected by unsuitable storage conditions, dust, contamination, or rough handling. Frames and finished lenses can also become scratched, bent, or damaged when they are not stored securely or given enough protection.
Review the full movement of materials through the lab, starting when a delivery arrives. Check how items are transferred into storage, how they are organised and protected, and how they are later moved from the storage area to the production floor.
Look for risks such as:
- Unprotected lenses placed on hard surfaces
- Materials stacked incorrectly
- Trays that are damaged or unsuitable
- Dust or residue in storage areas
- Products stored outside recommended conditions
- Inconsistent cleaning procedures
- Frequent manual transfers between containers
- Poor separation of completed and unfinished work
Handling rules should be easy to follow during busy periods. A process that depends on employees remembering several exceptions is more likely to fail when order volume increases.
Maintain and Calibrate Equipment Proactively
Production equipment can continue to run even when it is no longer working as accurately as it should. Instead of causing one clear breakdown, this gradual change may lead to a slow increase in damaged or defective lenses.
Regular preventive maintenance can help the lab find and correct these issues before they affect a larger number of jobs. Maintenance schedules should follow the equipment manufacturer’s recommendations, but they should also consider the lab’s own production and defect data.
Machines that process large numbers of lenses, operate for long periods, or handle more demanding materials or jobs may need to be cleaned, inspected, and calibrated more often.
A maintenance programme should consider:
- Cleaning schedules
- Calibration checks
- Tool and consumable replacement
- Coolant condition and filtration
- Chuck, block, pad, and clamp condition
- Pressure and temperature settings
- Relevant machine settings
- Software and firmware updates
- Inspection of moving or high-wear components
- Documentation of faults and repairs
Compare maintenance activity with defect data wherever possible. This makes it easier to see whether cleaning, repairs, part replacements, or recalibration have improved production quality.
For example, if the defect rate falls after a worn component is replaced or a machine is recalibrated, the lab can use that result to plan future maintenance more effectively. It may show that the equipment should be checked or serviced sooner, before the same problem develops again.
Operators should also be trained to recognise the early signs of equipment trouble. Changes in sound, vibration, cycle time, lens position, or surface finish may indicate that a machine needs attention. Reporting these signs early can prevent a minor issue from damaging a larger number of lenses.
Control Process Settings
The same machine settings will not produce the best results for every type of lens. A lens can react differently during production depending on its material, prescription strength, design, coating, thickness, and the conditions inside the lab. Using the wrong pressure, speed, temperature, tool, or production cycle can increase the risk of chipping, cracking, changing shape, or developing surface damage.
Test and record the settings that work best for common product combinations. Staff should be able to access these instructions easily, while only authorised employees should be allowed to change approved machine settings.
When settings are adjusted, record:
- What was changed
- Why it was changed
- Who approved the change
- Which jobs were affected
- Whether the change improved the result
When introducing a new lens material, design, coating, or treatment, test it under controlled conditions before using it in full production. Record the settings, results, defects, and any changes made during these trials.
Initial testing may require extra time and materials, but it is usually far less expensive than finding the same process problem after it has affected a large number of customer orders.
Standardise Work Between Operators and Shifts
If the outcome of the same job changes depending on who completes it, the production process may not be consistent enough. Clear written procedures should explain the main steps, quality checks, machine settings, and handling requirements for each stage of production. These instructions should be easy to find in the area where the work is performed. They should also be reviewed and updated whenever equipment, materials, or production processes change.
Pictures, diagrams, and examples can make instructions easier to follow. They are especially useful for tasks involving lens positioning, tool selection, inspection standards, or assessing whether a lens meets the required quality standard.
Standard procedures do not replace employee experience or judgement. Instead, they give every employee the same reliable starting point and reduce unnecessary differences in how jobs are handled.
Managers should also compare defect rates and production results across teams and shifts. If one shift has fewer defects, its working methods may include a useful technique that can be introduced elsewhere. A higher defect rate may point to missing training, an uneven workload, limited access to equipment, or differences in supervision.
Train Staff to Prevent and Identify Defects
Quality control should be part of every production stage, not only the final inspection. Every employee who handles or processes a lens should understand the problems that can happen during their part of the process. They should know how to prevent common defects, how to recognise signs of damage, and which checks must be completed before the lens moves to the next stage.
Employees should also know when to stop a job and report a problem. Passing a damaged or incorrect lens forward only adds more labour, machine time, and materials to a job that may eventually need to be started again.
Training should include:
- Correct material handling
- Equipment setup and approved settings
- Cleaning requirements
- Identification of common defects
- Inspection methods and tolerances
- Escalation procedures
- Accurate use of defect codes
- Safe responses to equipment warnings
- Recording unusual events or production issues
Include real examples of defects found in the lab when training employees. Physical samples and clear images are often easier to understand than written descriptions alone. They help staff see the difference between normal variation and a genuine quality problem that requires action.
Training should not be treated as a one-time activity. Review and update it whenever the lab introduces new equipment, materials, products, or production processes. Additional training may also be needed when the data shows an increase in a specific type of defect.
Improve Quality Control Without Creating a Bottleneck
Adding more inspections does not always lead to better quality. If staff repeatedly check every lens without a clear purpose, the process can slow down production without solving the problem that caused the defect.
Instead, place inspections at the production stages where errors or damage are most likely to occur. These checks should help the lab find problems before more time, labour, and materials are spent on a lens that will eventually fail.
For example:
- Verify job and material details before production starts
- Check critical measurements after generating or polishing
- Inspect surfaces before coating
- Confirm shape, axis, and size after edging
- Inspect for mounting damage before dispatch
- Complete a final check against the original order
Combining well-placed inspections with automated routing and production visibility can help the lab find problems earlier without creating unnecessary delays between production stages.
Automated inspection tools can make quality checks faster and more consistent, but they should not replace good process control. Detecting a defective lens quickly is useful, but improving the production process so the defect does not happen in the first place provides greater value.
Use Data to Prioritise Improvements
When the lab records many different types of defects, it can be difficult to know which problems should be addressed first.
Begin with the defects that have the greatest effect on production, costs, turnaround times, and customers. These will not always be the problems that happen most often.
For example, a defect that occurs only occasionally may still be a high priority if it affects expensive lenses, requires several production steps to be repeated, or leads to urgent shipping costs. In some cases, this type of failure can cost the lab more than a common breakage involving a lower-cost lens.
Rank problems according to:
- Frequency
- Material cost
- Labour and machine time
- Effect on turnaround
- Customer impact
- Risk of recurrence
Then investigate the most important category in detail.
For each recurring defect, ask:
- Where was the problem found?
- Where was it most likely introduced?
- Which products, machines, or processes are involved?
- When did the rate begin to change?
- What conditions were present at the time?
- Has the same issue occurred before?
- What action would prevent another occurrence?
Avoid closing an investigation after replacing the failed lens. A remake solves the immediate order but does not correct the process that caused it.
Monitor Whether Corrective Actions Work
Every improvement should have a responsible owner, a clear deadline, and a result that the lab can measure.
For example, if the lab changes an edging setting to reduce chipping, compare the chipping rate before and after the adjustment. If employees receive new training on handling lenses, monitor the related defect categories across different teams and shifts. If a supplier replaces a faulty batch of materials, continue tracking those materials to confirm that the problem has been resolved.
If a corrective action does not improve the results, review it and decide what needs to change. Do not continue using the same approach simply because it has already been introduced.
Managers should receive regular quality reports that show current defect rates, changes over time, serious incidents, and the progress of ongoing improvement work. Production teams should also have access to the results that relate to their work. This helps make quality part of everyday lab operations instead of a topic discussed only by management.
Reliable reporting is especially important when production information is spread across several systems. When moving optical operations to cloud-based software, labs should confirm that historical quality records, equipment connections, reporting rules, and audit trails will remain complete and accessible after the transition.
Questions to Ask About Your Current Process
When investigating lens defects and breakage, ask:
- Do we record every defect using consistent reason codes?
- Can we identify the machine, material, operator, and production stage involved?
- Are we recording where defects originate or only where they are found?
- Which defect categories create the highest total cost?
- Have failure rates changed by product, supplier, machine, or shift?
- Can we compare equipment maintenance records connected to production results?
- Can staff access current work instructions at each production stage?
- Are new materials and processes tested before full production?
- Do corrective actions have owners and measurable targets?
- Can customer service see accurate remake and completion information?
- Can we access quality reports available without assembling data manually?
- Can we confirm that a process change actually reduced the problem?
If several of these questions cannot be answered, the lab may need better data and workflow visibility before it can achieve a sustained reduction in defects.
Make Quality Part of the Production Workflow
Reducing lens defects and breakage rates is not a single quality-control project. It is the result of consistent data, controlled processes, reliable equipment, effective training, and clear accountability.
The strongest labs do more than count failed lenses. They connect each defect to the order, material, machine, production stage, and underlying cause. They then use that information to prevent the same problem from happening again.
A connected optical production platform can support this approach by tracking every job, standardising defect records, connecting quality results with production activity, and making performance visible across the lab.
To explore how better workflow control and production visibility could support your operation, discuss your optical lab requirements with Ocuco.